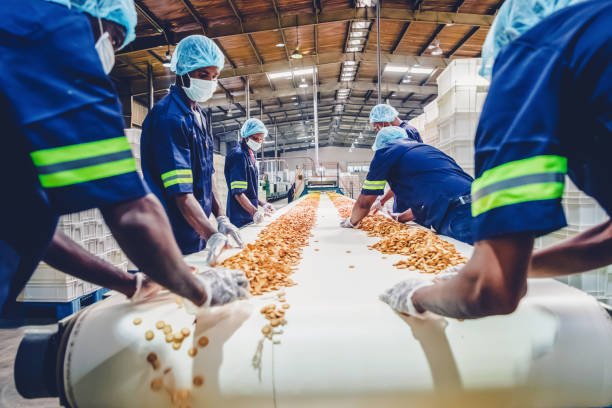
Golden Oil industries is hiring a refinery supervisor in Onitsha, Anambra State.
Job Summary
To direct shift-level oil refining operations, including degumming, neutralization, bleaching, and deodorization, leading operators and technicians to hit volume targets, minimize material waste, ensure equipment availability, and uphold strict product quality standards.
Responsibilities
Supervise Operations: Oversee all phases of the refining process, including degumming, neutralization, bleaching, and deodorization.
Team Leadership: Lead, train, and mentor production staff to ensure a high level of performance and adherence to safety and quality standards.
Quality Control: Monitor product quality throughout the refining process, conducting regular inspections and tests to ensure compliance with industry standards and specifications.
Production Planning: Collaborate with the production manager to develop and implement production schedules, ensuring efficient use of resources and meeting production targets.
Safety Compliance: Promote a culture of safety, ensuring that all operations comply with health and safety regulations. Conduct regular safety audits and training sessions.
Process Improvement: Identify opportunities for process optimization and efficiency improvements. Implement changes to reduce waste and increase yield.
Inventory Management: Oversee inventory levels of raw materials and finished products, ensuring timely replenishment and minimal disruption to production.
Reporting: Maintain accurate records of production metrics, quality tests, and safety incidents. Prepare regular reports for management.
Safety Briefings & Toolbox Talks: Conduct mandatory daily safety pre-shift briefings (Toolbox Talks) with operators and technicians to communicate task-specific hazards, high-risk operational alerts, and required safety precautions.
Workplace Hazard Identification & Shift Safety Audits: Lead daily shift floor walks to identify and eliminate unsafe behaviors, ergonomic hazards, trip/slip risks, and unguarded machinery across all active processing areas.
Permit-to-Work (PTW) & Isolation Enforcement: Authorize and verify Permit-to-Work (PTW) requirements—including Lockout/Tagout (LOTO) verification and hot work clearances—before allowing team members or maintenance crews to work on energized, pressurized, or high-temperature machinery.
PPE & Safety Standard Compliance Monitoring: Enforce total adherence to Personal Protective Equipment (PPE) mandates and safety protocols across all shift personnel, taking immediate corrective or disciplinary action in cases of non-compliance.
Shift Incident & Near-Miss Investigation: Lead immediate initial investigations for all shift-level safety incidents, injuries, near-misses, or unsafe conditions, reporting root causes and corrective action plans to plant management and the HSE team.
Shift Emergency Response & Evacuation Direction: Serve as the designated primary shift floor warden during plant emergencies, directing safe machine shutdown sequences, managing orderly floor evacuations, and leading headcounts at assembly points.
Substance & Chemical Spill Mitigation Leadership: Direct the immediate containment, cleanup, and area isolation during chemical or high-volume vegetable oil spills on the production floor, ensuring proper disposal of contaminated cleanup materials.
Requirements
A Bachelor’s (B.Eng. /B.Sc. / HND) degree in Sciences or Social Science is required for this role.
5 to 10 years proven production work experience preferably in the food Manufacturing Sector of which having a minimum 5years in Supervisory capacity.
Deep knowledge of production management and Experience in reporting on key production metrics
Proficient in MS Office.
Familiarity with HACCP, ISO, GMP, AND Personal hygiene compliance Guidelines.
Experience and knowledge of provincial health and safety standards.
Knowledge of project management principles and good housekeeping practices.
Knowledge of business and management principles and practice.
Excellent supervision, communication (oral and written), business presentation, skills, Organization, and leadership abilities, Self-motivated with a result driven approach, Problem- solving skill.
Benefits
Pension, HMO, leave Allowance, Canteen, transportation, performance incentives, etc
How to Apply
Apply for this role using this link
Secondary Keywords: